Copper Rod Continuous Casting
and Rolling Line
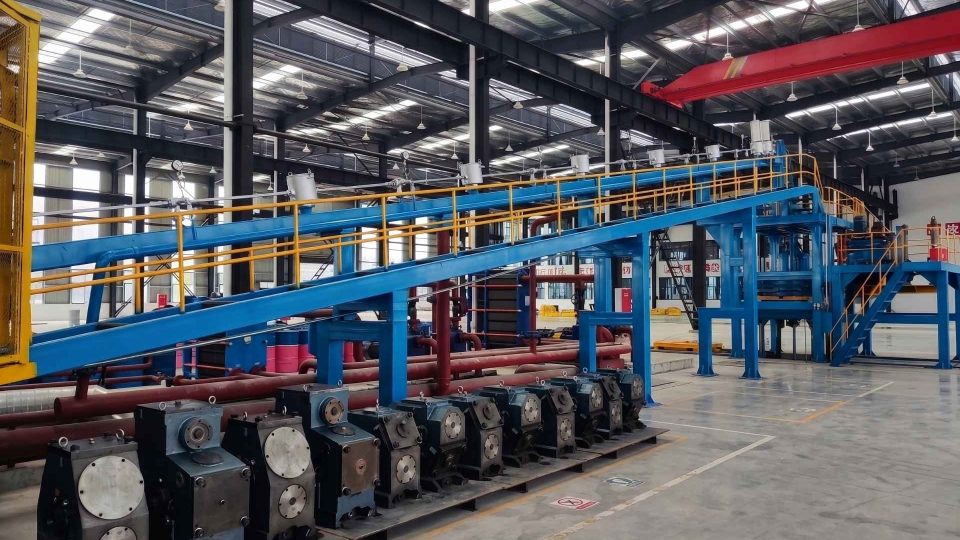
Our UL+Z line produces coiled copper rod from electrolytic copper (ETP) or scrap-derived FRHC feedstock. It combines melting, continuous casting, hot rolling, cooling and collection in a line configured for your rod specification and production requirements.
Key Features
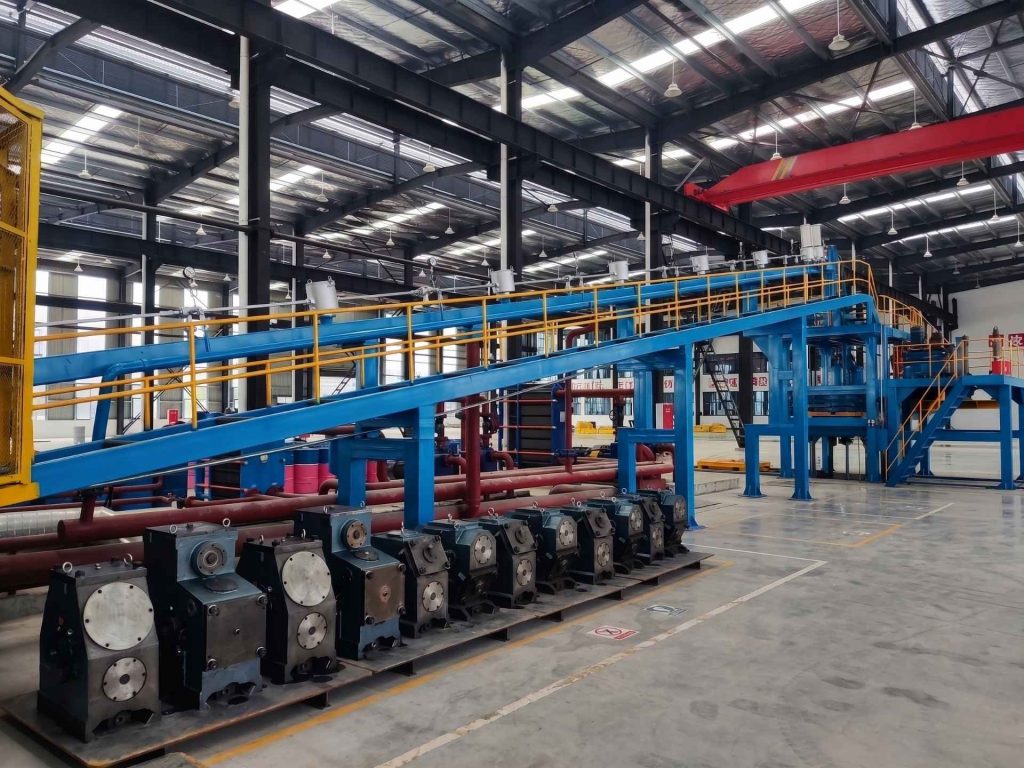
• Furnace packages can be arranged for electrolytic copper or scrap-derived FRHC feedstock.
• The five-wheel casting machine supplies a continuous billet to the rolling section.
• Active feeding and rod-stacking parking functions help manage material flow through the mill.
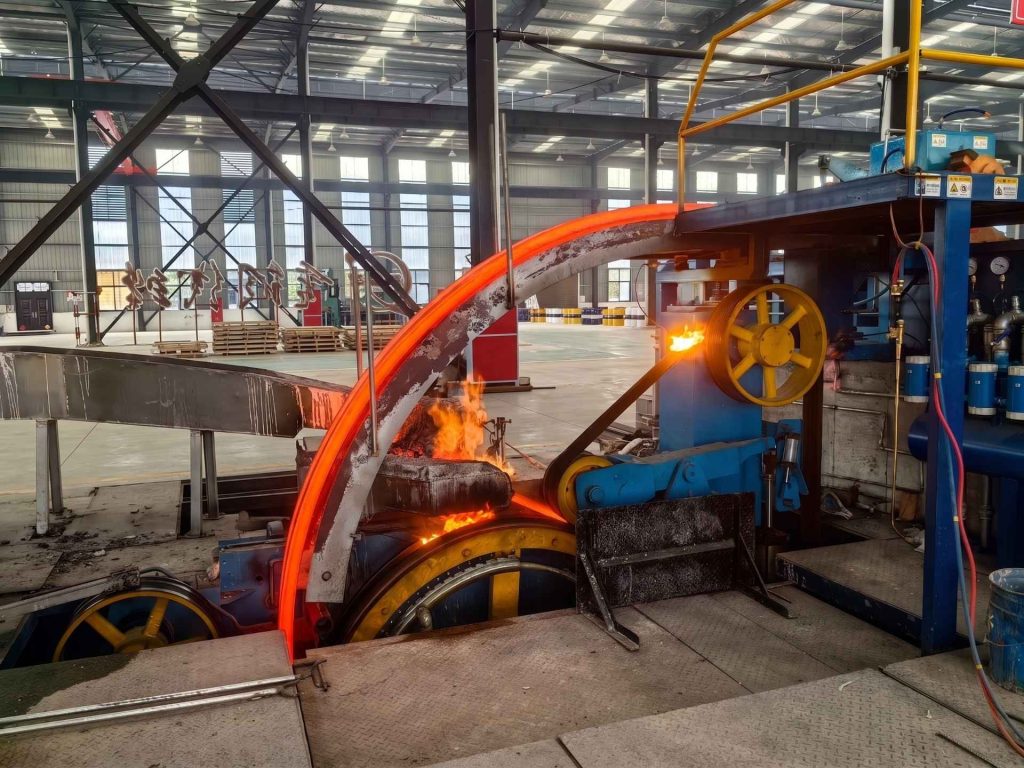
• Two-roller and three-roller deformation stages are combined to develop the required rod geometry and drawing performance.
• Cooling, reduction and rod collection are coordinated with the selected output and package.
Equipment Composition
• Vertical furnace and holding furnace (for electrolytic copper) or reverberatory furnace (for scrap copper)
• Five-wheel integral continuous casting machine
• Rolling shear
• Straightening machine
• Roughing machine
• Continuous rolling mill
• Lubrication system
• Cooling and reduction device
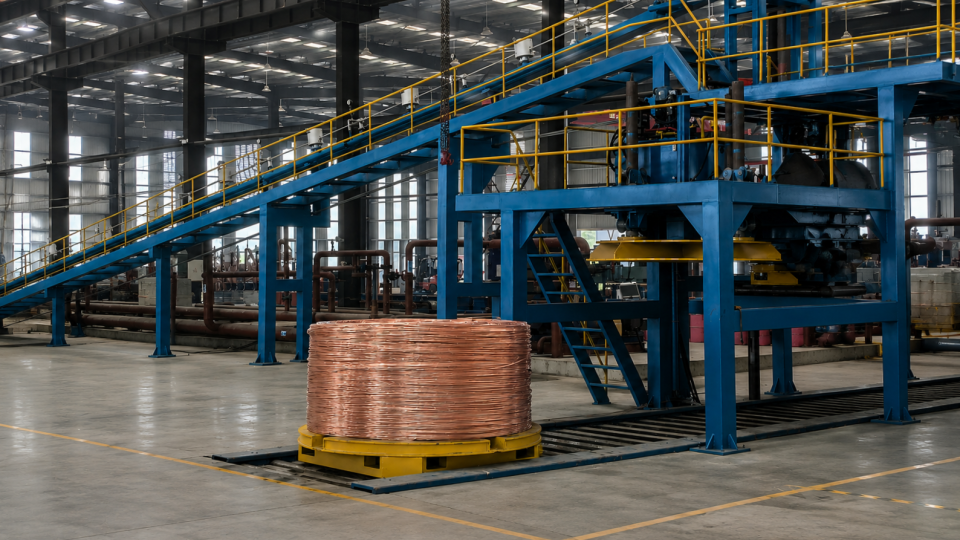
• Rod collection device
• Electrical control system
Technical Parameters
| Model | Product Diameter (mm) | Crystal Wheel Diameter (mm) | Casting Area (mm²) | Stand Form | Rolling Speed (m/min) | Output (t/h) | Total Power (kW) |
|---|---|---|---|---|---|---|---|
| UL+Z-1900/8+255/4+8 | 8, 10, 12.5, 16 | 1900 | 2300 | 4+8 | 9.6 | 14–16 | 650 |
| UL+Z-2100/8+330/2+255/4+8 | 8, 10, 12.5, 16 | 2100 | 3800 | 2+12 | 11 | 14–18 | 800 |
| UL+Z-2100/8+330/3+255/2+8 | 8, 10, 12.5, 16 | 2100 | 3200 | 3+10 | 11 | 14–18 | 800 |
| Model | Product Diameter (mm) | Crystal Wheel Diameter (mm) | Casting Area (mm²) | Stand Form | Rolling Speed (m/min) | Output (t/h) | Total Power (kW) |
|---|---|---|---|---|---|---|---|
| UL+Z-2100/20+330/2+255/6 | 16, 20 | 2100 | 3800 | 2+6 | 9.6 | 14–18 | 800 |
| UL+Z-2100/30+330/3+255/6 | 16, 20, 25, 30 | 2100 | 3800 | 3+6 | 9.6 | 14–18 | 850 |
What Determines Line Performance
ETP and FRHC production have different melting requirements, so we select the furnace system for the feedstock first. Its melt rate must match the casting section, rod diameter, rolling stands, cooling capacity and collection method. Copper quality and the conditions at the plant also influence the operating duty.
The technical tables show reference configurations. We confirm the proposed output and finished-rod requirements against the complete line, including the interfaces between melting, casting, rolling and collection.
Suitable Feedstock
Electrolytic copper (ETP) and scrap-derived FRHC feedstock are the two principal routes in our current range. For copper-alloy applications, we confirm the composition, melting practice and rolling behavior separately.
Typical Applications
Coiled copper rod for wire and cable, electrical conductors and downstream drawing plants. The finished rod specification should be agreed with the next process rather than treated as an isolated product.
Planning a Copper Rod Line
Start by telling us the copper feedstock you plan to use, the rod you want to produce and the installation country. Share a target output if you have one. As the project develops, we confirm the ETP or FRHC route, rod diameter, drawing duty and coil format, then review furnace fuel, power, cooling water, layout, environmental controls and destination standards with your team.
From Process Data to Technical Proposal
We review the feedstock, product and site data before recommending the furnace package, casting section, rolling arrangement and supply boundary. In our proposal, we identify the reference configuration, principal utilities and items that still require confirmation.
If the route is still being compared, see the Copper Processing Lines guide.
See how a casting and rolling line works in practice in our Nanchong copper rod project, or browse Projects & Insights for more project updates.